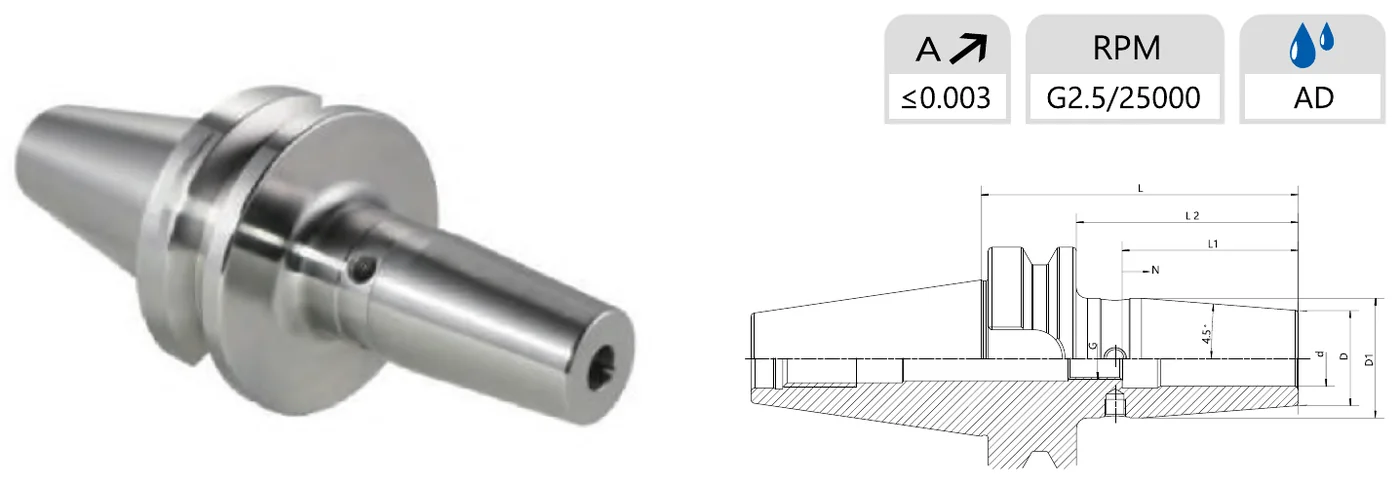
The bore is heated by induction until it grows a few hundredths of a millimetre, the tool shank drops in, and the bore contracts onto it as it cools. Nothing else is in the joint — no collet, no nut, no wedge. The holder and tool behave as one body.
Three consequences follow, and they are the reason shrink fit is standard practice in high-speed and mould work: the highest clamping force available per unit of holder diameter; the slimmest possible nose profile, so the holder reaches into cavities other chucks cannot; and nothing that can move out of balance, which is what allows run-out ≤ 0.003 mm and G2.5 balance at 25,000 rpm.
| Shank | Standard | Through coolant | Interface |
|---|---|---|---|
| BT | 122 article numbers → | 63 article numbers → | BT (MAS 403 BT, 7/24 taper) |
| BBT | 76 article numbers → | 63 article numbers → | BBT (dual-contact BIG-PLUS style face-and-taper) |
| SK | 106 article numbers → | 58 article numbers → | SK / DIN 69871 (ISO 7/24) |
| CAT | 82 article numbers → | 72 article numbers → | CAT / ANSI-ASME B5.50 (ISO 7/24) |
| HSK-A | 147 article numbers → | 67 article numbers → | HSK form A (DIN 69893-1) |
| HSK-E | 50 article numbers → | — | HSK form E (DIN 69893-5, symmetric, high speed) |
| HSK-F | 44 article numbers → | — | HSK form F (DIN 69893-6, symmetric, wood/high speed) |
Pick the bore to match the tool shank exactly — a shrink fit bore is sized to one nominal diameter, there is no clamping range. Then pick the shortest gauge length that still reaches the feature: every millimetre of unnecessary projection costs stiffness, and stiffness is what shrink fit is bought for.
For reach, balance and rigidity, yes — there is nothing in the joint. Against that, each bore holds exactly one shank diameter and you need an induction unit to change tools. Hydraulic chucks damp vibration better and change tools with a key; collet chucks cover a range per holder. Most shops run shrink fit for high-speed, deep-cavity and finishing work and keep collet or hydraulic for general milling. Mongtec publishes all three — see all tool holder types.
Bores are ground to suit h6 tool shanks. Send the actual shank tolerance if your tools are not h6 and Mongtec confirms the bore before quoting.
Yes. Non-standard gauge lengths and shank interfaces are made to drawing — send the drawing or the machine and the reach you need.
Send the spindle interface, the tool shank diameters you run and the reach you need. Dimensioned drawings are supplied by email once the enquiry is open.
All tool holders · Quick-change clamping · All Mongtec article numbers